
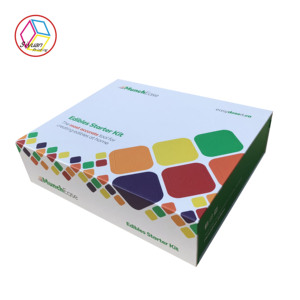
Custom 2mm Rigid Kraft Board Pharma Box with Gloss Lamination
Ultra-dense 2mm greyboard construct with glossy moisture-barrier lamination. Eco-friendly recyclable kraft backing for OTC presentation suites.
Get a QuoteExplore our Health Canada-aligned custom rigid packaging portfolio designed specifically for pharmaceutical clinical trials, biological therapeutics, OTC product lines, and luxury medical devices in Toronto and the GTA region.
Ultra-dense 2mm greyboard construct with glossy moisture-barrier lamination. Eco-friendly recyclable kraft backing for OTC presentation suites.
Get a Quote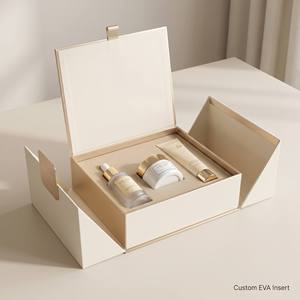
Dual-opening magnetic flap equipped with high-density anti-static EVA foam die-cut specifically for vial holding, syringes, and clinical ampoules.
Get a Quote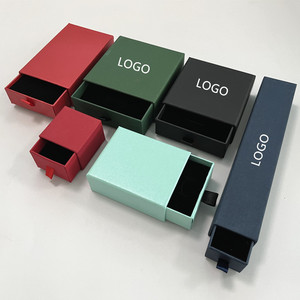
Heavy-duty sleeve and drawer mechanism crafted from recycled rigid greyboard. Ideal for specialty prescription packaging and diagnostic test kits.
Get a Quote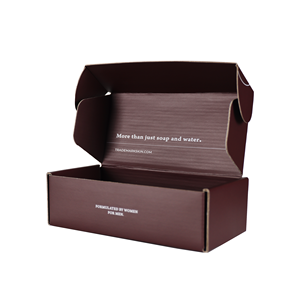
Re-enforced micro-flute rigid mailer designed for temperature-controlled cold chain logistics throughout Ontario's pharmaceutical supply routes.
Get a Quote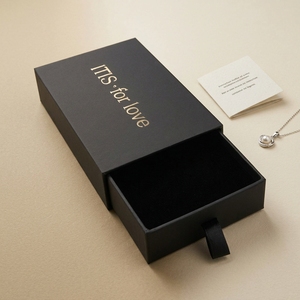
Smooth friction-fit pull drawer rigid container wrapped with anti-bacterial coated paper. Secure storage for clinical trial blister packs.
Get a Quote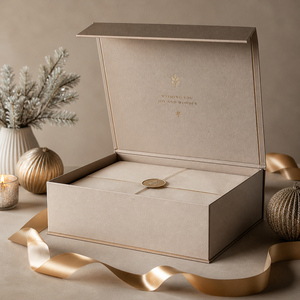
Space-saving flat-folding rigid box with integrated magnetic catch seal. Reduces warehouse storage volume by 70% before final package assembly.
Get a Quote
Classic telescope lid-and-base rigid setup engineered for diagnostic hardware, surgical tools, and premium dermatological sample packaging.
Get a Quote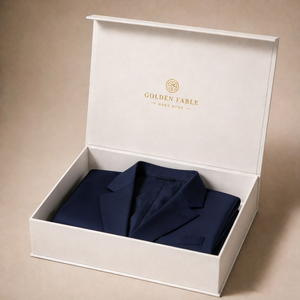
Sleek matte black wrapped setup box with heavy magnetic closure and customized velvet-laminated foam cavity for biological samples.
Get a QuoteThe Greater Toronto Area (GTA)—anchored by major pharmaceutical clusters in Mississauga’s "Pill Hill", Markham’s biotech corridors, and Downtown Toronto’s Innovation District—represents Canada’s primary biopharmaceutical manufacturing and distribution gateway. In this highly regulated ecosystem, secondary and tertiary packaging does far more than enclose a product. It serves as a critical guardian of drug stability, regulatory compliance, brand authenticity, and patient safety.
Unlike standard folding paperboard cartons, custom rigid boxes (also termed set-up boxes) are constructed from thick, high-density greyboard cores ranging from 1.5mm to 3.0mm (800 to 1800 GSM). Wrapped in specialized coated sheets, anti-bacterial films, or eco-conscious kraft paper, rigid boxes provide an unyielding structural envelope that prevents crushing, shields against ambient thermal spikes, and guarantees tamper-evident delivery from cleanroom production lines to hospitals, clinics, and retail pharmacies across Ontario.
Our custom rigid pharma box manufacturing processes adhere strictly to Health Canada’s Good Manufacturing Practices (GMP) Division 2 guidelines, as well as international ISO 15378 standards (primary packaging materials for medicinal products with specific reference to GMP). Every production run destined for the Toronto market undergoes rigorous physical testing, including edge-crush test (ECT) validation, ISTA 3A transit simulation, and VOC outgassing checks to safeguard sensitive active pharmaceutical ingredients (APIs).
Precision biopharmaceutical packaging demands rigorous material selection. Toronto biopharmaceutical procurement officers must evaluate multiple structural variables when specifying rigid boxes for high-value biologicals, injectable suites, diagnostic kits, and expensive clinical trial supplies.
Integration of destructive paper tear-seals, serialized hologram labels, breakable magnetic latches, and tamper-indicating covert spot UV print layers preventing illicit diversion and package counterfeiting.
Precision CNC waterjet-cut medical EVA foam, cross-linked polyethylene (XLPE), anti-static molded pulp, and thermoformed PET trays designed to hold ampoules, vials, syringes, and auto-injectors without displacement.
Specially coated metallic paperboard wraps, barrier varnishes, and insulated vacuum-panel lining options engineered to support +2°C to +8°C cold chain stability during GTA ambient temperature fluctuations.
For biopharmaceutical logistics managers in Ontario, choosing between standard folding cartons and custom engineered rigid packaging boils down to structural risk, presentation value, and product fragility:
| Packaging Feature | Custom Rigid Pharma Boxes | Standard Folding Cartons | Regulatory / Operational Benefit |
|---|---|---|---|
| Structural Density | 1.5mm - 3.0mm Solid Greyboard Core | 0.3mm - 0.6mm Paperboard | Zero crushing under pallet stacking weight; protects fragile glass vials. |
| Transit Damage Rate | < 0.02% (ISTA 3A Tested) | ~ 1.85% under heavy stress | Ensures high-cost therapeutics arrive intact at hospital delivery bays. |
| Insulation Thermal Retention | High (Multi-layered thermal barrier) | Low (Rapid thermal loss) | Extends gel-pack cold chain buffer during GTA winter/summer transit spikes. |
| Security & Lock Integration | Child-Resistant (CRSF) & Magnetic Locks | Tuck-in flaps / simple glue seals | Meets ASTM D3475 child resistance standards for controlled substances. |
| Unboxing & Branding Impact | Executive Presentation & Clinical Luxury | Standard Commodity Feel | Critical for physician sample kits, launch kits, and patient onboarding. |
Pharmaceutical, biotechnology, and medical technology companies operating within Toronto and surrounding regional hubs leverage custom rigid boxes across distinct high-value applications:
In the pharmaceutical supply chain, lead-time bottlenecks can stall critical clinical trial phases or cause stock-outs at retail pharmacies. Working with a dedicated packaging partner supplying the Toronto market guarantees rapid prototyping within 48 hours, localized inventory buffering in GTA warehouses, and compliance with Canadian bilingual packaging regulations (English/French text rendering under Health Canada GUI-0001).
As Toronto expands its status as a global biotechnology powerhouse, the demand for next-generation rigid pharmaceutical packaging is accelerating along three key axes:
Ontario healthcare institutions and pharmaceutical conglomerates are enforcing strict ESG (Environmental, Social, and Governance) targets. Modern custom rigid pharma boxes utilize 100% post-consumer recycled (PCR) greyboard cores, bound by soy-based water-soluble inks and bio-laminations. This eliminates petroleum-derived plastic wraps without compromising the box's structural rigidity or cleanroom sterility requirements.
The integration of RFID tags, NFC temperature logging sensors, and dynamic 2D DataMatrix codes directly into the rigid box structure allows pharmaceutical distributors in Mississauga and Vaughan to monitor real-time location, opening events, and thermal exposure history throughout Ontario’s logistics routes.
Balancing child safety with senior accessibility (CRSF standards) remains a regulatory focus in Canada. Advanced rigid boxes now incorporate hidden dual-push release buttons, squeeze-and-slide drawer locks, and magnetic sequence latches that require specific hand dexterity, ensuring safety in homes while remaining easy to open for elderly patients managing chronic health conditions.
With over two decades of technical expertise in custom packaging structural design, our facility stands as a premier supply partner for Toronto’s demanding healthcare and biopharmaceutical sectors. Our enterprise advantages include:
Yes. Our custom rigid pharma packaging is designed and manufactured in accordance with Health Canada’s Good Manufacturing Practices (GMP) Division 2 requirements and ISO 15378 standards. We ensure strict raw material selection, non-toxic food-and-pharma grade adhesives, low-VOC soy inks, and bilingual (English/French) typographic layout support.
We provide precision-engineered custom inserts including medical-grade high-density EVA foam, anti-static cross-linked polyethylene (XLPE), recyclable molded paper pulp, rigid corrugated dividers, and clear thermoformed PET trays. Each insert is custom-milled to lock vials, syringes, or diagnostic components firmly in place during air or ground freight across Canada.
We offer 3D digital CAD dieline mockups within 24 hours. Once dielines are approved, unprinted physical structural prototypes (blank CAD samples) can be produced and delivered to your office in Toronto, Mississauga, Markham, or Brampton within 48 to 72 hours. Production-grade pre-press color proofs take approximately 5 business days.
Absolutely. To combat pharmaceutical counterfeiting, we integrate covert UV ink patterns, serialized tamper-evident seal stickers, micro-text graphics, custom-branded security holograms, tamper-indicating breakable closures, and embedded RFID/NFC chips directly into the rigid board structure.
We accommodate both low-volume clinical trial needs and large-scale commercial manufacturing. Our standard low MOQ starts at just 250 units for custom rigid setup boxes, allowing biopharmaceutical startups and clinical research institutions in Ontario to order exact quantities without overcommitting inventory capital.
Our high-density greyboards (up to 3.0mm thickness) possess natural insulating properties superior to thin paperboard folding cartons. Combined with moisture-resistant outer laminations (matte/gloss/anti-scratch) and internal thermal barrier liners, our rigid boxes maintain structural rigidity without warping when transferred between ambient room temperatures and cold storage rooms (+2°C to +8°C or ultra-cold gel pack containers).
Partner with Toronto’s trusted custom rigid pharma box manufacturers. Get instant technical consultation, custom CAD dielines, and competitive enterprise pricing today.